Skip to content

Built for how your sector runs

Shop floor data you can act on today

We build production tracking, machine monitoring, quality and maintenance software that connects your shop floor to ERP and gives plant heads live numbers.

Digital tools for the factory floor

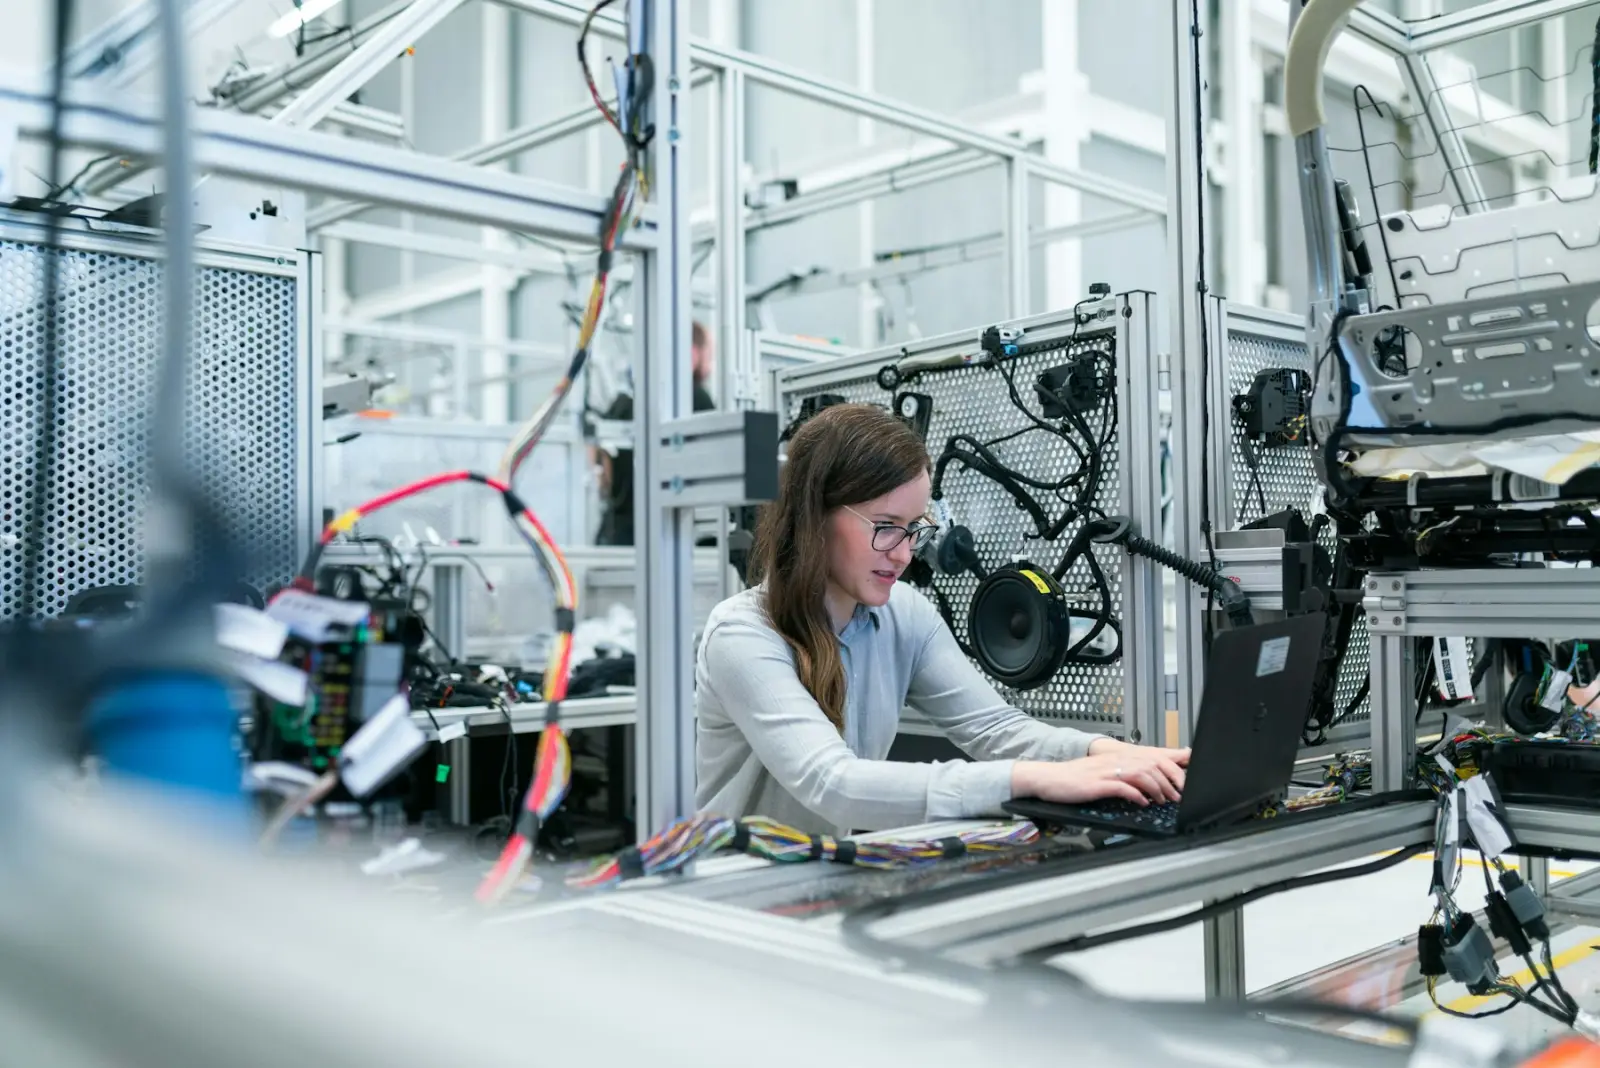
Many factories run a capable ERP for finance and purchasing, while the shop floor still runs on paper job cards, whiteboards and end-of-shift spreadsheets. By the time a plant head sees yesterday's output, downtime causes and rejection rates, the chance to fix today's shift has gone. That gap between the shop floor and the office is where most manufacturing software delivers value.

We work with discrete and process manufacturers, auto component makers, pharma and FMCG plants, engineering firms and contract manufacturers. Typical needs are production planning and tracking, machine monitoring through PLCs or IoT sensors, quality inspections, maintenance management, material traceability and dealer or distributor portals connected to the ERP you already run.

Nexzem starts on the floor with operators and supervisors, because tablet screens that slow them down will not be used. We connect machines through standard protocols such as OPC UA and MQTT where possible, and integrate with SAP, Tally, Oracle or custom ERPs. Dashboards focus on OEE, downtime reasons and quality trends.

What manufacturing teams get with Nexzem

Scroll along the line: each outcome lights up as the signal reaches it.

  1. Same-shift decisions

    Live data lets supervisors fix stoppages and quality drift before the shift ends.

  2. Less paperwork

    Digital job cards and checklists remove manual data entry and transcription errors.

  3. Audit-ready traceability

    Every batch links to materials, machines and inspections for customer and regulatory audits.

  4. ERP stays the record

    We extend your ERP rather than replace it, protecting existing investments.

Manufacturing software we build

MES, IIoT dashboards, quality and maintenance software for factories and industrial manufacturers.

Manufacturing execution systems

Work orders, routing, operator logins, production counts and shift reports that track every job from release to finished goods.

Every build includes

  • Same-shift decisions
  • Less paperwork
  • Audit-ready traceability
  • ERP stays the record

Standards and compliance on the factory floor

Manufacturing software often has to produce evidence for audits. ISO 9001 expects controlled documents and quality records, automotive suppliers working to IATF 16949 need traceability and control of nonconforming parts, and pharmaceutical and medical device makers serving the US must meet FDA 21 CFR Part 11 for electronic records and signatures, with EU GMP Annex 11 playing a similar role in Europe.

Architecture standards help too. The ISA-95 model describes how enterprise systems such as ERP and plant systems such as MES and SCADA should divide responsibilities and exchange data, and the ISA/IEC 62443 series addresses industrial cybersecurity. This is general information, not legal or certification advice; quality and regulatory teams should confirm requirements for each product and market.

In practice, compliance features should be part of the design rather than added before an audit. Record who did what and when for every critical step, prevent edits to approved records except through controlled corrections, and make reports easy to export in the format auditors request.

  • Keep audit trails for every change to production and quality records.
  • Use electronic signatures with identity checks where regulations require them.
  • Link each batch or serial number to materials, machines and operators.
  • Control document versions for work instructions and specifications.
  • Segment plant networks and restrict remote access.
How to choose a manufacturing software partner

Factory software succeeds when it fits real shift work. A strong partner spends time on the shop floor, talks to operators and supervisors as well as managers, understands industrial protocols such as OPC UA and Modbus, and designs screens for gloves, noise and bright lighting. They should be comfortable working alongside your ERP vendor and maintenance team rather than replacing everything.

Ask for a pilot with measurable goals on one line before plant-wide rollout, and for clarity on who supports the system during night shifts. Plants cannot wait until morning when a production terminal stops working, so support hours, spare devices and offline behavior must be agreed upfront.

  • Which machine protocols and PLC brands have you connected?
  • How will the system behave if the network drops mid-shift?
  • What does success look like for the pilot line?
  • How do you integrate with our ERP without duplicating data?

Where AI fits in manufacturing

Proven uses include predictive maintenance from vibration, temperature and current data, camera-based quality inspection that catches defects consistently across shifts, process parameter optimization that improves yield, and demand forecasting that feeds production planning. Maintenance assistants grounded in equipment manuals and past work orders help technicians diagnose faults faster.

Data readiness decides success. Many plants first need reliable machine data collection, consistent downtime reason codes and labeled defect images before models can learn anything useful. Start where the cost of the problem is clear, such as a bottleneck machine or a high scrap rate, and compare model recommendations against experienced engineers before automating decisions.

How we build for manufacturing

Clear stages with a review at the end of each, so you always know what happens next and what it costs.

  1. 01

    Plant visit

    We walk the line with operators, supervisors and maintenance to see real constraints.

  2. 02

    Connectivity assessment

    We check machine controllers, network and sensors to plan data capture.

  3. 03

    Pilot on one line

    One line or cell goes live first, proving value and refining screens.

  4. 04

    Plant-wide rollout

    Modules extend to other lines and integrate fully with ERP.

  5. 05

    Continuous improvement

    We review dashboards with your team and add reports and alerts as needs evolve.

Manufacturing use cases

  1. Shift-wise OEE for injection molding

    Machine signals capture cycle counts and stoppages automatically, operators tag downtime reasons on a terminal, and supervisors see availability, performance and quality for every machine during the shift instead of the next morning.

  2. Batch genealogy for a pharma plant

    Every batch record links raw material lots, equipment, operators, in-process checks and approvals with electronic signatures, so quality teams can trace or recall a batch in minutes and present complete records during inspections.

  3. Tool life tracking for CNC machining

    The system counts tool usage per machine and part, alerts operators before tools reach their limit and records tool changes, reducing broken tools, scrapped parts and unplanned stops on high-value machining jobs.

  4. Supplier quality portal

    Suppliers submit inspection reports and certificates before dispatch, the plant records incoming inspection results and raises corrective actions online, and purchasing sees supplier quality ratings when placing new orders or renewing contracts.

  5. Energy use per unit produced

    Smart meters on major machines and utilities feed a dashboard showing energy consumed per part or batch, highlighting idle running and inefficient shifts so the plant can cut power costs and report emissions accurately.

Technology behind our manufacturing software

Proven, well-supported tools chosen for your scale, budget and team, never for novelty.

  • React
  • Angular
  • Python
  • Node.js
  • .NET
  • PostgreSQL
  • Grafana
  • Azure
  • Docker
  • Pandas

Manufacturing software FAQs

Something else on your mind? Ask a consultant and get a reply within one business day.

What does manufacturing software cost?

Cost depends on the number of lines and machines, whether machines need new sensors or gateways, the modules required and ERP integration complexity. We share a fixed quote after a free consultation, usually starting with a pilot line.

Can you connect older machines?

Often yes. Older machines without network ports can be monitored with add-on sensors, current transducers or PLC gateways. We assess each machine type during the plant visit.

Do you replace our ERP?

No. We integrate with your ERP and build shop floor tools around it. The ERP remains the system of record for finance, purchasing and inventory.

Can the system run on our own servers?

Yes. We deploy on premises, in the cloud or in a hybrid setup where shop floor data is collected locally and summarised to the cloud.

How long does an MES or monitoring pilot take?

A pilot on one line usually takes 8-12 weeks, including hardware setup. Plant-wide rollout follows in phases.

Can you support FDA 21 CFR Part 11 for electronic records?

Yes. We design systems with secure user authentication, electronic signatures linked to records, complete audit trails, controlled access and record retention, and document validation activities. Your quality team remains responsible for the validation strategy, and we provide the evidence and documentation it needs.

Can operators use the software in noisy, dirty shop floor conditions?

Yes. We design large touch targets that work with gloves, high-contrast screens readable under factory lighting, barcode and RFID scanning to avoid typing, and visual and audible alerts. Rugged tablets or industrial terminals are recommended where devices face dust, oil or impact.

We work with clients across the USA, UK, Australia, UAE, New Zealand and India.

Where we work

Software that fits how your sector works.

Share your workflows and compliance needs. We reply within one business day with a suggested approach and team.